16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 469 |
Published by VMT at Oct 14 2026 | Reading Time:About 6 minutes


Precision-machined metal components are a popular choice due to their high precision, dimensional stability, and a wide selection of surface finishes and treatments. However, these metal products often require a surface identification process, such as company logos, critical part numbers, batch codes, or 2D barcodes (QR codes) for traceability, which is essential for modern manufacturing and quality control. For custom metal component projects, metal laser engraving has become a highly favored solution. Unlike traditional stamping, chemical etching, or ink printing, laser engraving delivers micron-level precision, exceptional durability, and complete design flexibility without compromising the structural integrity of precision-machined parts. In this comprehensive guide, we will break down everything you need to know about metal laser engraving for custom CNC parts, including: core working processes and parameters, compatible vs. hard-to-engrave metals, engraving effects, depth control, surface finish considerations, and practical applications.
At the end of this article, we will also share a case study: manufacturing custom wear-resistant stainless steel drive shafts for automation machinery, followed by multi-pass high-power fiber laser deep engraving. This process creates a stable, micron-level physical recess depth on the stainless steel surface, ensuring long-term legibility even under severe friction and wear.
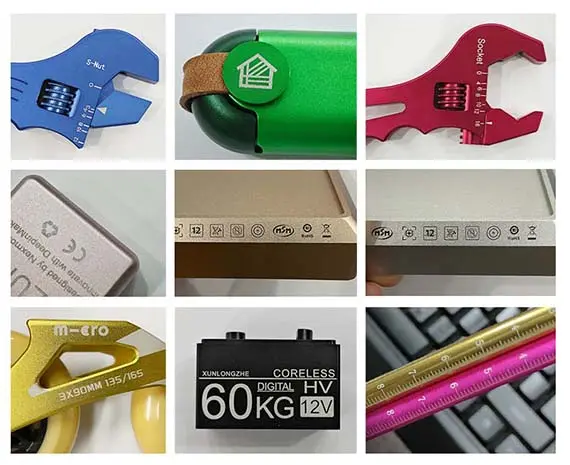
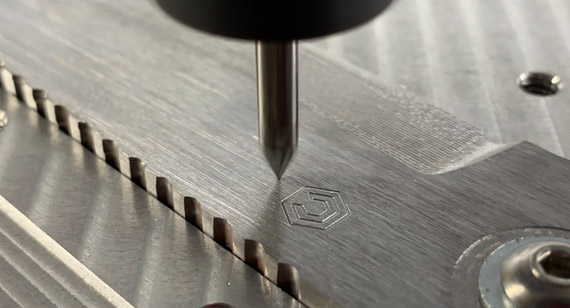
Metal laser engraving is a non-contact manufacturing process that utilizes a high-power focused laser beam to physically remove, melt, or alter the surface layer of a metal workpiece. This creates permanent, high-contrast impressions, cavities, or surface markings.
When applied to custom CNC machined parts, such as aluminum housings, stainless steel brackets, or titanium aerospace components, laser engraving serves several essential functions:
Unlike:
Metal laser engraving vaporizes or ablates microscopic layers of metal. This leaves a distinct, tactile, and permanent recess to achieve the traceability and identification mentioned above.
Yes, but long-term legibility depends heavily on engraving depth and process parameters.
In environments subject to continuous mechanical friction, heavy oil contamination, or abrasive wear (such as drive shafts, industrial gears, or high-touch components), superficial laser markings (depths under 0.005 mm) can fade over time as the base surface wears down.
Engraving Depth; Solutions in Our Factory
The laser engraving process on metal parts involves a precise digital-to-physical workflow. While hobbyists might use CO₂ lasers for simple projects, engraving components for industrial applications should always be handled by a professional one-stop factory specializing in CNC machining, surface finishing, and metal laser engraving.
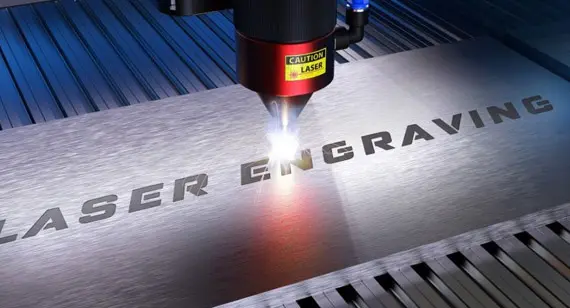
Below is an overview of the workflow when laser engraving metal parts:
Step 1: CAD and Vector Graphic Preparation
The process begins by exporting specific graphic requirements into vector formats (such as DXF, DWG, AI, or SVG). Because vector graphics use mathematical paths rather than pixels, the laser control software can map exact coordinate vectors (X and Y axes) across complex 3D contours or flat surfaces.
Step 2: Fiber Laser System Selection
Industrial metal laser engraving utilizes fiber lasers (typically operating at a wavelength of ~1,064 nm). Metallic surfaces absorb this wavelength exceptionally well, enabling high-energy transfer, deep penetration, and razor-sharp focal points.
After machining custom parts and completing any required surface finishing for our clients, our CNC facility uses fiber lasers to engrave custom markings. We avoid CO₂ lasers because their longer wavelength (~10,600 nm) is largely reflected by metallic surfaces rather than absorbed. This leads to poor energy efficiency and risks creating blurry, ill-defined engravings.
Step 3: Non-Contact Thermal Ablation Process
Once the component is securely clamped in the laser marking station, the fiber laser beam is directed by high-speed galvo-mirror scanners:
When selecting metal laser engraving for custom CNC parts, material choice directly influences not only the visual contrast and durability, but also processing efficiency and cost.
For the vast majority of standard CNC machined metals (like standard aluminum and stainless steel), laser engraving setup times and processing costs remain very similar and budget-friendly. However, choosing hard-to-process or highly reflective metals requires specialized laser sources, complex parameter tuning, or multi-pass setups, which significantly increases machine cycle time and engineering costs.
Easy-to-Engrave Metal Materials
Metals like stainless steel (304, 316, 17-4 PH), titanium alloys, aluminun, and tool steels are ideally suited for fiber laser engraving. They possess high thermal absorption at standard 1,064 nm wavelengths and lower thermal conductivity, allowing optical energy to vaporize the surface cleanly without excessive heat bleed. These materials yield crisp contrast, ranging from deep physical grooves to jet-black laser annealing, with fast cycle times and minimal setup adjustments.
Hard-to-Engrave Metal Materials
Materials such as pure copper, brass, and bronze fall into the challenging category. Due to their high thermal conductivity, heat rapidly dissipates away from the laser focus point, making localized physical ablation much harder to achieve. Additionally, their high optical reflectivity can bounce laser light back into the galvo optical head, requiring precise pulse modulation, specialized anti-reflective lenses, and higher energy outputs to carve crisp lines.
Unsuitable Metal Materials for Laser Engraving
Metals with extremely low melting points or toxic/corrosive surface contaminants are generally unsuitable for direct industrial laser engraving. For example, lead and cadmium-bearing alloys pose severe health risks when vaporized into hazardous fumes during laser ablation. Furthermore, thin-plated metals with inconsistent plating thickness can peel, flake, or discolor unpredictably under intense thermal shock, making mechanical engraving or pad printing a safer alternative.
How to Handle High-Reflectivity Metals (Copper and Brass) ?
To safely and cost-effectively engrave highly reflective metals without damaging optic systems, our facility deploys short-pulse MOPA (Master Oscillator Power Amplifier) fiber lasers. By using ultra-short pulse durations and high peak energy, the laser vaporizes the metal substrate faster than heat can dissipate. We also adjust focal offsets and polarization angles to maximize optical absorption and minimize dangerous back-reflection.
How to Handle Anodized Aluminum and Powder-Coated Metal Parts?
Post-treated metal parts offer fantastic visual contrast when laser engraved:
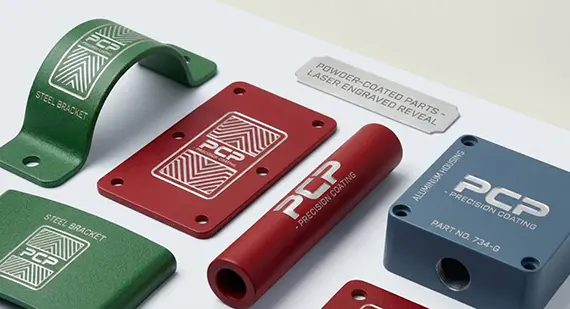
Summary Table for Laser Engraved Metal Materials
| Material Category | Examples | Compatibility Level | Typical Visual Result | Cost and Cycle Time Impact |
| Easy-to-Engrave Metals | Stainless Steel (304/316), Titanium, Tool Steel, Carbon Steel | High (Optimal) | Jet-black annealing, crisp frosted marks, or deep physical grooves | Standard / Cost-Effective (Fast setup and quick cycle time) |
| Pre-Treated Surface Metals | Anodized Aluminum, Powder-Coated Steel / Aluminum | High (Optimal) | High-contrast white/bright metal logos on colored background | Standard / Cost-Effective (Low power needed, fast ablation) |
| Hard-to-Engrave Metals | Pure Copper, Brass, Bronze, Raw Bare Aluminum | Moderate (Requires Expertise) | Dark brown, frosted, or golden engraved lines | Higher Cost (Requires MOPA lasers, multi-pass setups, slower speed) |
| Unsuitable / High-Risk Metals | Lead, Cadmium Alloys, Thin/Inconsistent Plated Metals | Low / Unsuitable | Toxic fumes, peeling, flaking, or uneven burn marks | Not Recommended (Requires alternative marking methods like CNC carving) |
Metal laser engraving is widely utilized across demanding manufacturing industries thanks to its duribilty and long-term functional identification. Here are the most common applications:
Part Identification and Complete Traceability
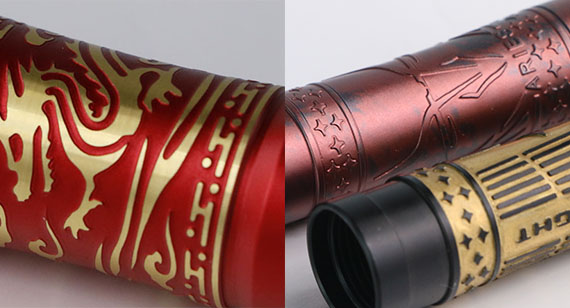
Branding and Aesthetic Customization
Functional and Operational Markings
Anti-Counterfeiting and Security Marking
Micro-engraving covert security marks, unique identification cryptographic keys, or tiny holographic patterns onto expensive custom metal components to safeguard intellectual property and prevent counterfeit replacements.
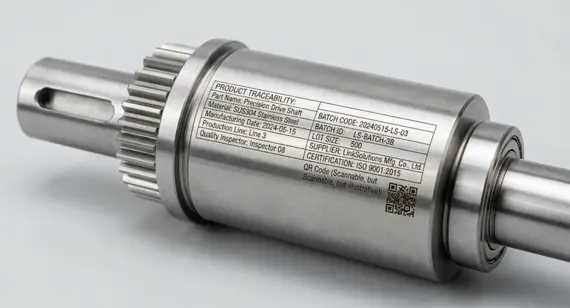
Multi-pass laser deep engraving on custom stainless steel drive shafts ensuring long-term legibility even under friction and wear.
A leading European automation equipment manufacturer partnered with us to produce custom 316L stainless steel drive shafts for high-speed robotic assembly lines. Operating continuously in heavy-oil, high-friction, and high-temperature environments, these shafts required permanent serial numbers, QR codes, and alignment calibration marks. Traditional laser marking or ink printing was unsuitable, as superficial marks quickly worn off under severe mechanical friction, leading to lost component traceability.
We began by turning and grinding the 316L stainless steel shafts on multi-axis CNC lathes to achieve a strict dimensional tolerance of ±0.005 mm and a mirror-like surface roughness of Ra 0.4 μm. Because 316L stainless steel possesses high toughness and corrosion resistance, maintaining precise geometry prior to laser processing was essential to ensure uniform laser focal distance across the cylindrical surface.
To achieve maximum durability without introducing micro-cracks or thermal distortion to the drive shaft, our engineers deployed a 50W MOPA fiber laser system. Rather than relying on a single high-energy pass, which risks thermal warping, we executed a optimized multi-pass ablation strategy (12 sequential high-speed passes at 1,064 nm wavelength). This created a clean, burr-free physical recess with an exact depth of 0.035 mm into the stainless steel substrate, far exceeding standard surface wear allowances.
Following laser deep engraving, the drive shafts underwent chemical passivation (ASTM A967) to rebuild the protective chromium oxide film inside the engraved micro-grooves, restoring the corrosion resistance. Optical profilometer inspection confirmed crisp edge definition and fully scannability for the micro QR codes. Field tests demonstrated that even after 2,000 hours of continuous high-load frictional operation, the physical recess depth remained fully legible and intact, successfully fulfilling the client’s strict long-term traceability standard.
Metal laser engraving is a versatile, highly durable, and precise surface-identification solution that plays a critical role in modern precision manufacturing. From deep physical recession engraving on wear-resistant CNC drive shafts to clean, high-contrast branding on anodized aluminum housings, laser engraving provides permanent traceability without compromising component tolerances. Whether you need standard logo marking or complex multi-pass deep engraving for harsh industrial environments, selecting the right process, depth, and material strategy is essential for controlling production time and costs.
Need to test laser durability or contrast on your machined metal components before mass production? From deep multi-pass engraving for high-wear parts to precision marking on anodized surfaces, our machining factory delivers custom DFM feedback and rapid prototyping. Upload your drawings to optimize your part's finish and cost today! [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, metal material, surface finish, engraving content, required depth, tolerance requirements, prototype quantity and production quantity. VMT will review CNC machining, surface finishing, laser engraving, inspection and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
1. Is it possible to remove laser engraving from metal parts?
A: Yes, but the removal method depends on the engraving type. Shallow laser annealing or surface marking (under 0.005 mm) can be removed by light surface grinding, mechanical polishing, or re-anodizing. However, multi-pass deep physical engraving (0.02 mm+) requires precision CNC re-machining, heavy grinding, or bead blasting, which removes base material and will alter the local dimension of the part.
2. How do laser engraving removal methods compare in terms of surface impact?
A: Common removal methods compare as follows:
3. Will removing a laser engraving affect critical CNC part dimensions and tolerances?
A: Yes. Removing deep laser engraving requires removing the surrounding metal down to the bottom of the recessed groove. For example, removing a 0.03 mm deep engraving requires taking off at least 0.03–0.05 mm of material. If the area falls within a tight tolerance zone (such as a bearing fit with ±0.005mm allowance), removing the engraving will push the part out of spec.
4. How much extra turnaround time does laser engraving add to a batch of 2,000 CNC machined parts?
A: For a standard production batch of 2,000 CNC metal components (engraving simple logos, serial numbers, or 2D matrix codes), the laser engraving cycle time is typically only 15 to 30 seconds per part. Adding standard laser engraving to a 2,000-piece production run adds roughly 2 to 3 working days to the overall lead time, including machine setup, batch handling, and inspection.
5. Should laser engraving be done before or after heat treatment and passivation?
A: Generally, laser engraving is performed after final heat treatment to prevent high-temperature scaling or oxidation from obscuring the mark. For stainless steel, we recommend performing passivation after laser deep engraving to ensure the protective chromium oxide film is fully restored within the freshly engraved micro-grooves.
6. Can you laser engrave text or serial numbers onto curved or cylindrical metal parts?
A: Yes. By integrating 4th-axis rotary fixtures or 3D dynamic galvo-focusing heads, the fiber laser systems can automatically adjust focal length in real time to engrave seamless text, logos, and barcodes around cylindrical components like shafts, valves, and bushings.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more