16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 533 |
Published by VMT at Oct 21 2026 | Reading Time:About 5 minutes


In the field of CNC machining, cutting aluminum is a crucial technique. Aluminum, known for its light weight, high strength, and corrosion resistance, is widely used in industries such as aerospace, automotive, and electronics. This article provides a detailed overview of 12 professional methods and techniques for CNC cutting aluminum, aimed at helping readers better master the manufacturing technology of aluminum CNC machined parts, improving production efficiency and product quality.
Additionally, this article covers the challenges and solutions for different grades of CNC cut, thermal expansion control, residual stress mitigation, as well as professional CNC machining techniques. At the end of the article, we will also share a case study on precision robotic articulated finger components, demonstrating how we solved joint backlash and achieved tight +/-0.008 mm tolerances with a Ra 0.4 µm surface finish for our client.
Before CNC cutting aluminum, it's essential to understand the characteristics of aluminum and CNC machining equipment. Aluminum has excellent thermal conductivity and ductility but also has a relatively soft texture and high thermal expansion coefficient. Therefore, selecting appropriate tools, cutting parameters, and cooling fluids is crucial when CNC cutting aluminum. Additionally, ensuring equipment maintenance and tool management is necessary for quality and safety during the machining process.
Choosing the Right Tools: Select tools with high hardness, wear resistance, and good cutting performance, such as carbide or high-speed steel tools, based on the characteristics of aluminum.
Optimizing Cutting Parameters: Set reasonable cutting speeds, feed rates, and cutting depths based on the hardness and thickness of the aluminum to improve machining efficiency and surface quality.
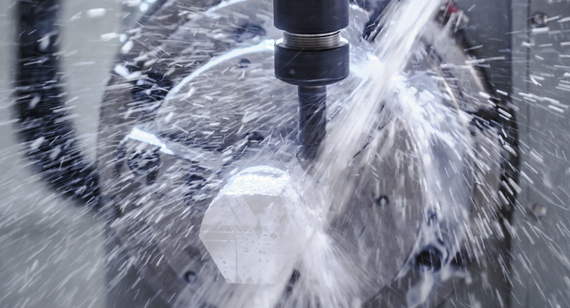
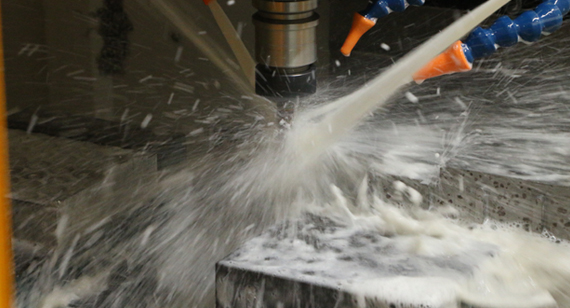
Using High-Pressure Coolant: Employing high-pressure coolant can effectively reduce cutting temperature, minimize tool wear, and prevent workpiece deformation.
Reverse Cutting: Use reverse cutting, which involves turning both sides of the aluminum workpiece, to reduce the formation of long, stringy aluminum chips.
Increasing the Number of Tools: Increase the number of tools to achieve more efficient machining, such as using multiple tools simultaneously to enhance production efficiency.
Controlling Cutting Depth: Control the cutting depth to avoid excessive cutting, which can damage tools or deform the workpiece.
Optimizing Tool Paths: Optimize tool paths based on the shape of the aluminum and machining requirements to reduce idle running and unnecessary cutting, thus improving efficiency.
Selecting Appropriate Cutting Lubricants: Cutting lubricants play a role in cooling, lubricating, and cleaning during CNC cutting. Choosing the right lubricant can enhance machining efficiency and surface quality.
Controlling Cutting Temperature: Monitor cutting temperature closely during CNC cutting. Excessive temperatures can soften and deform aluminum and cause tool wear.
Regular Tool Wear Inspection: Regularly inspect tool wear and replace severely worn tools promptly to ensure machining quality and efficiency.
Using CNC Prototyping Technology: CNC prototyping technology can quickly and accurately produce aluminum prototypes, providing a reliable basis for subsequent mass production.
Providing Customized CNC Machining Services: Offer customized CNC machining services, including cutting, drilling, and milling aluminum, based on specific customer requirements to meet personalized needs.
CNC cutting aluminum technology is widely used in various industries. For instance, in the automotive industry, aluminum is used to manufacture engine and body parts. In the electronics industry, aluminum is used for heat sinks and enclosures. In the aerospace industry, aluminum is used for aircraft and rocket components. Additionally, CNC cutting aluminum technology plays a significant role in construction and shipbuilding.
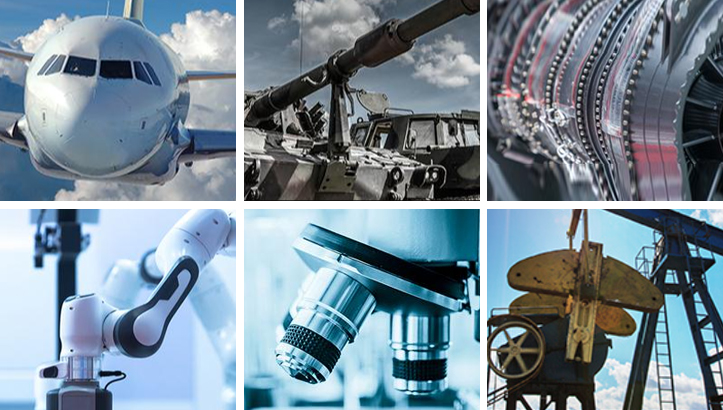
Manufacturing factories typically perform CNC aluminum cutting based on your industry and specific aluminum product requirements to meet custom performance and aesthetic needs. Here are several common applications and CNC aluminum cutting techniques:
CNC cutting aluminum technology offers advantages such as high precision, high efficiency, and high flexibility, meeting the needs of various industries for aluminum processing. Additionally, the exceptional thermal conductivity and light weight of aluminum make these precision-cut components ideal for weight-sensitive applications. Furthermore, advanced CNC techniques ensure repeatable dimensional accuracy and superior surface finishes, significantly reducing secondary post-processing time.
However, it also faces challenges such as rapid tool wear, high cutting temperatures, and aluminum chip management. Therefore, practical application requires considering various factors and selecting appropriate methods and parameters to maximize the benefits of CNC cutting aluminum technology.
CNC Aluminum Machining Challenges and Actionable Solutions
| Cutting Challenge | The Cause | Practical Solutions |
| Material Sticking / Built-Up Edge (BUE) | Soft aluminum with high ductility combined with high cutting heat causes material to weld onto the tool tip and flutes. |
|
| Work Hardening | Localized plastic deformation during cutting causes a sudden increase in material surface hardness. |
|
| Burrs and Edge Flashing | High ductility causes the metal to drag or stretch rather than shear cleanly as the tool exits the part. |
|
| Part Warpage and Stress Deformation | Release of internal rolling/milling stresses or uneven heat distribution during machining. |
|
Aluminum is not a single, uniform material. It encompasses a wide variety of grades, each alloyed with different elements such as magnesium, silicon, copper, and zinc. These alloying elements significantly alter the hardness, ductility, melting point, and thermal conductivity of each grade. Read our guide on What is Aluminum to better understand the general properties and common grades of aluminum alloys.
When executing CNC cutting or machining on common aluminum grades, it is critical to understand their distinct material characteristics and specific cutting requirements to achieve optimal tolerances, surface finish, and tool life.
Table: Machining Characteristics of Aluminum Alloys
(These are also the ways how our factory CNC cut custom aluminum products for clients.)
| Aluminum Series and Grade | Machinability Rating | Challenges | What to Do? |
| 1xxx / 3xxx Series (e.g., 1060, 3003) |
Poor (Very Soft) | Tool sticking, Built-Up Edge (BUE), burr formation | High cutting speeds, strong coolant/lubrication, sharp single/double-flute polished end mills |
| 5xxx Series (e.g., 5052, 5083) |
Moderate | Work hardening, chip packing, moderate tool clogging | Maintain sufficient feed per tooth, avoid rub cutting, use high-pressure coolant for chip evacuation |
| 6xxx Series (e.g., 6061, 6082) |
Excellent | Thermal expansion affecting tight tolerances under prolonged high-speed machining | Standard aluminum cutting tools, high-speed machining, allow cooling time before finishing passes |
| 7xxx Series (e.g., 7075, 7050) |
Good | Rapid tool flank wear due to high hardness, part warpage from internal residual stress | Use coated (DLC) or PCD tools, symmetric material removal, stress-relief annealing steps |
1. 1xxx and 3xxx Series (Pure and Manganese-Alloyed Aluminum)
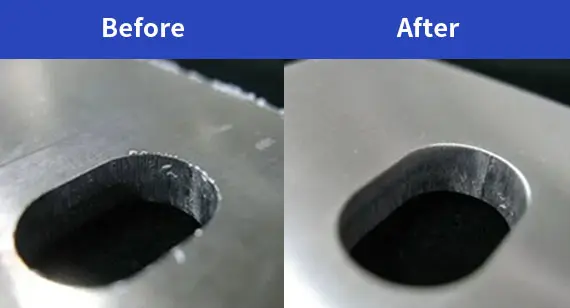
2. 5xxx Series (Magnesium-Alloyed Aluminum)
3. 6xxx Series (Magnesium-Silicon Alloyed Aluminum)
4. 7xxx Series (Zinc-Magnesium-Copper Alloyed Aluminum)
High-Precision CNC Cutting and Finishing for Robotic Articulated Finger Components to Achieve +/-0.008 mm Tolerance and Zero Backlash
A robotics developer approached us to manufacture aluminum finger links for their next-generation dexterous articulated hands. Their previous supplier failed to meet the stringent positional and dimensional tolerances required for the multi-axis joint assemblies. The initial parts suffered from cumulative dimensional errors exceeding +/-0.05 mm, causing noticeable joint play and mounting misalignment. To resolve these quality issues, we communicated thoroughly with the client to verify their project requirements, review the material recommended by the previous supplier, and pinpoint where the previous production fell short.
Upon evaluating the previous failure, we identified that unhandled material stress was contributing to part distortion. We recommended upgrading the material to stress-relieved 7075-T6 (T651) aluminum plate for its exceptional strength-to-weight ratio and dimensional stability, which the client approved. During the initial rough CNC milling pass, we utilized 3-flute carbide end mills with optimized chip-load parameters, leaving a precise 0.2 mm finishing allowance. The parts were then allowed to cool and equalize to room temperature, releasing localized cutting stress before moving to the high-precision finishing phase.
For the micro-finishing stage, we transferred the components to a climate-controlled 5-axis CNC machining center operating at a constant 20 °C. Using custom soft-jaw fixtures to prevent part distortion under clamping pressure, we applied custom diamond-coated (DLC) end mills to achieve exact pin-hole concentricity and flat mating surfaces. High-pressure flood coolant was continuously directed at the cutting zone to eliminate thermal expansion and flush away micro-chips, preventing any material re-welding or surface scratching. This setup held critical bore tolerances within +/-0.005 mm while maintaining a surface roughness of Ra 0.4 µm.
By combining precise DFM optimization, material upgrades, stress-relief milling cycles, and strict thermal control, we delivered 500 fully deburred, anodized finger module components with a 98% first-pass inspection rate. The client successfully assembled their robotic hands with zero joint backlash. Impressed by our ability to resolve the tolerance failures, the client has since designated our facility as one of their manufacturing partners for future robotic end-effector modules.
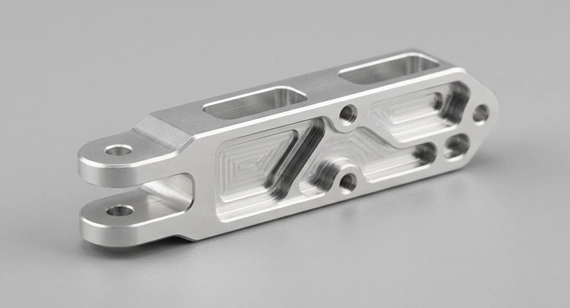
CNC cutting aluminum is a vital CNC machining technology with broad applications across many industries. This article introduces 12 professional methods and techniques for CNC cutting aluminum, aiming to help readers better master the manufacturing technology of aluminum CNC machined parts. In the future, with ongoing technological advancements and market development, CNC cutting aluminum technology will continue to improve and optimize, providing robust support for the growth of the aluminum machining industry. And, as industries demand tighter tolerances and more complex designs, mastering the nuances of different aluminum grades, managing thermal expansion, and controlling residual stresses will be essential. Ultimately, combining smart material selection with optimized milling strategies ensures higher efficiency, and excellent surface finishes.
Need help optimizing your aluminum parts for tight tolerances and zero burrs? Upload your drawings today for a free DFM review, and let our engineering team refine your design for rapid manufacturing. [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, aluminum grade, tolerance requirements, surface finish requirements, critical dimensions, prototype quantity and production quantity. VMT will review material selection, DFM, CNC machining, burr control, deformation control, inspection and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
Q1: What are standard CNC aluminum cutting tolerances?
A: Standard commercial tolerances for aluminum parts are typically ±0.005" (±0.125 mm) or ±0.002" (±0.05 mm). High-precision CNC cutting can achieve tight tolerances down to ±0.0005" (±0.013 mm) when controlled in a climate-conditioned environment with proper tooling.
Q2: What is the best tolerance for CNC aluminum parts?
A: The best tolerance is ±0.005" (±0.125 mm) for non-critical features, as it ensures high quality while keeping manufacturing costs low. For critical mating surfaces or bearing fits, a tolerance of ±0.001" to ±0.0005" (±0.025 mm to ±0.013 mm) is recommended.
Q3: How does aluminum stickiness affect custom part quality, and how is it controlled?
A: Soft aluminum grades can stick to cutting tools, causing rough surface finishes or tool breakage, which affects the surface quality and increases tooling fees for the aluminum products. To ensure flawless parts, we usually use polished, high-clearance cutters and high-pressure coolant to instantly clear chips before they heat up and weld to the tool.
Q4: How does aluminum thermal expansion affect CNC cutting?
A: Aluminum has a relatively high coefficient of thermal expansion (approx.
23×10 −6/K). Cutting heat causes the metal to expand during CNC cutting, which leads to dimensional errors once the part cools down. Mitigate this by roughing first, using heavy coolant, and letting the part cool to ambient temperature before taking final finish passes.
Q5: What is the best way to design aluminum parts to minimize deburring costs?
A: Adding small 0.2 mm to 0.5 mm chamfers or radii to sharp edges in your 3D CAD design allows the CNC machine to automatically debur edges during the milling cycle. This significantly reduces manual post-processing time and overall unit cost.
Q6: How do 6061 and 7075 aluminum compare in CNC cutting?
A: 6061-T6 is the most widely used grade, it offers excellent machinability, good surface finish, and cost-efficiency. 7075-T6 is much harder and stronger, producing short, clean chips with zero tool stickiness, though it causes faster mechanical tool wear and requires stress-relief strategies to prevent part warping.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more